
2,500 t / month
Lattice Towers & Structures
Lattice transmission towers, M-type towers and substation structures — cut, punched, formed, assembled and hot dip galvanized entirely in-house at 2,500 tonnes a month.
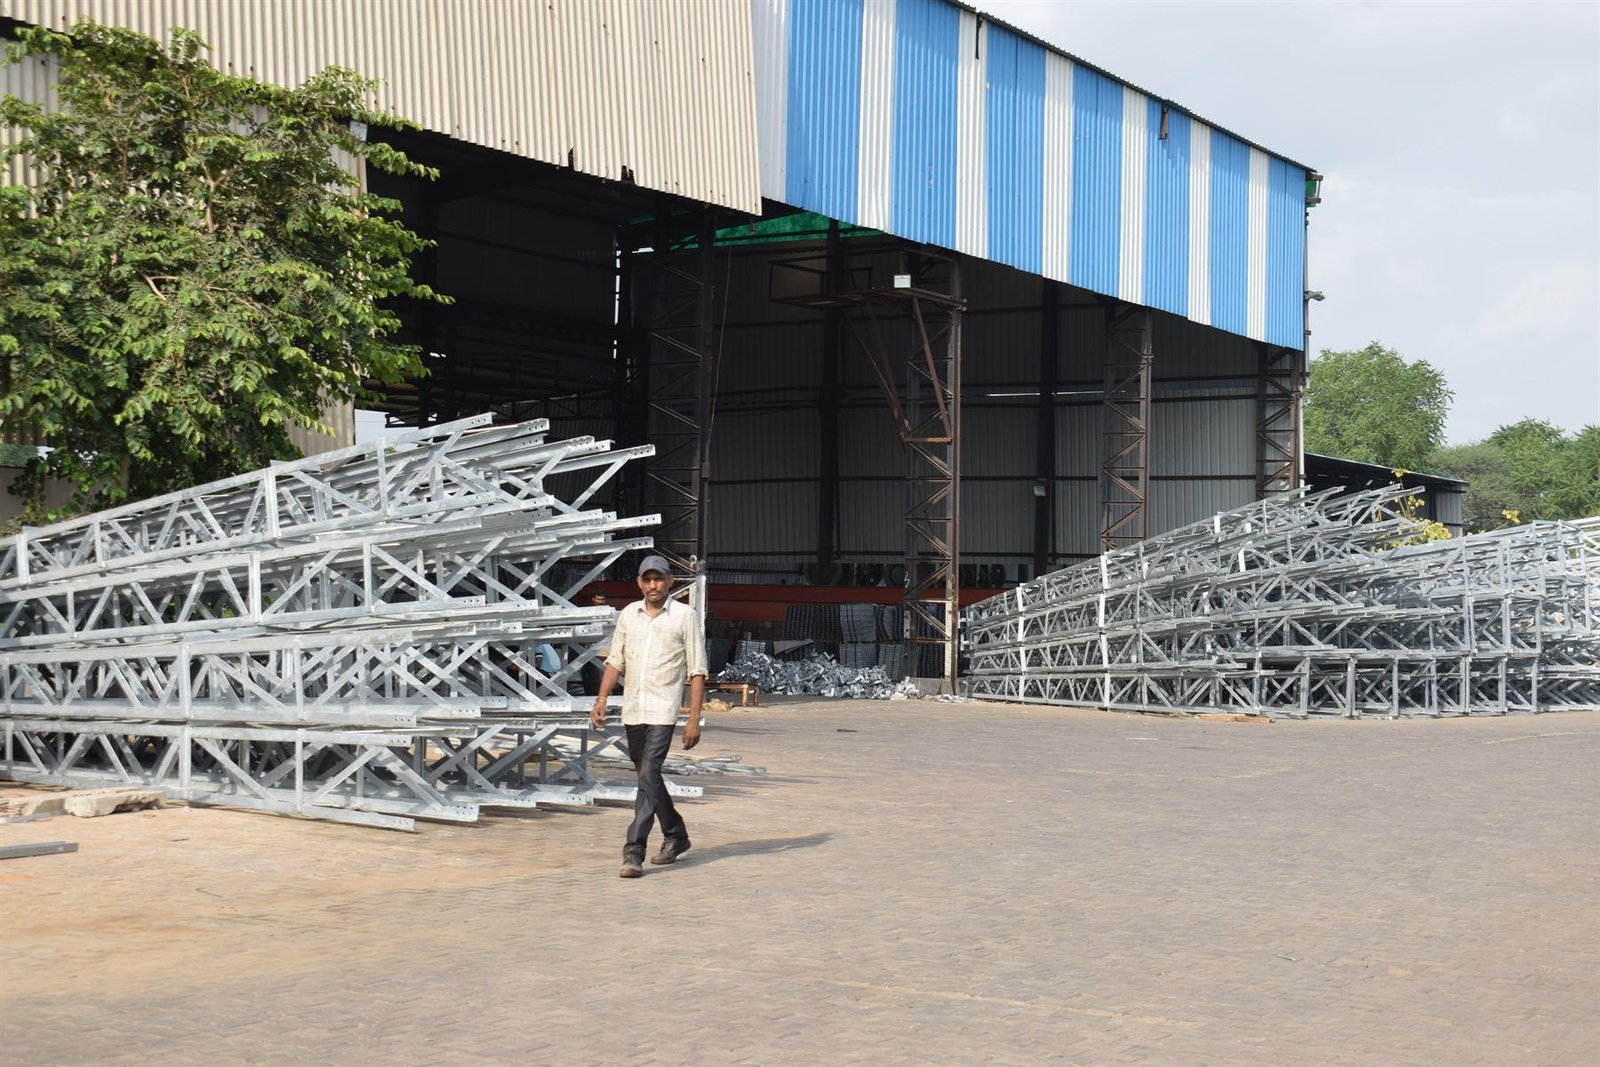
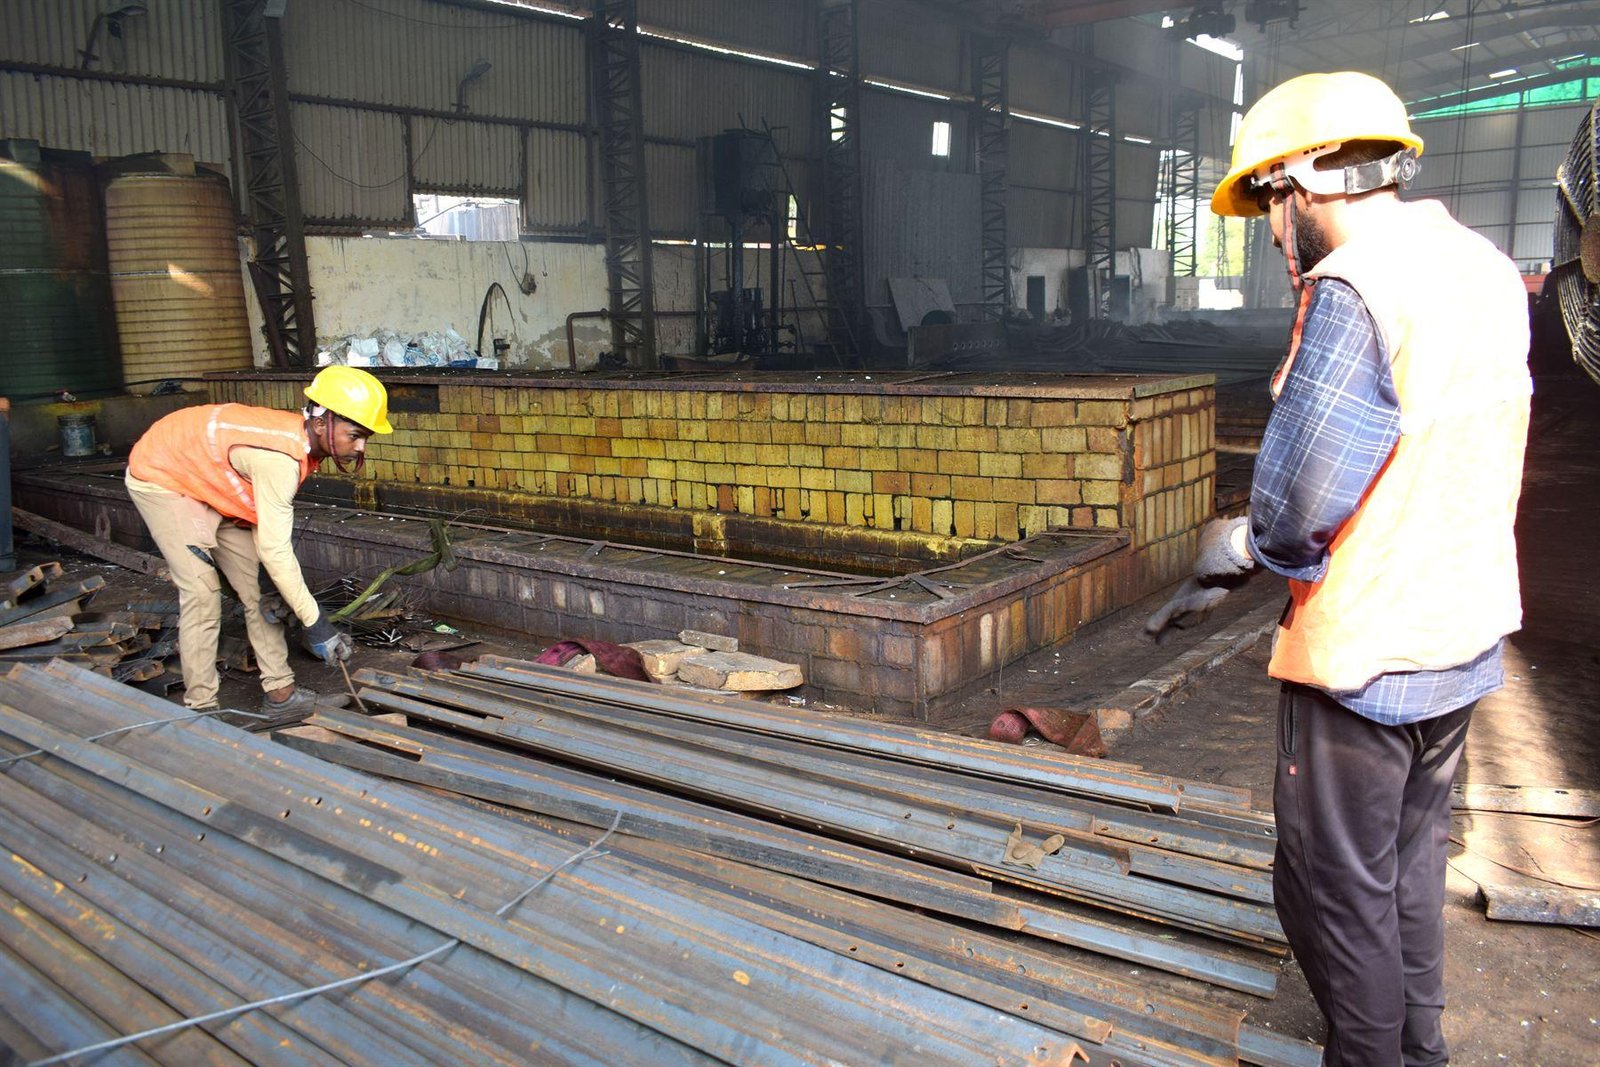
Galvanized tower sections leaving the shed
Overview
Sustained fabrication and galvanizing output.
No third-party coating queue in the delivery programme.
Fabrication against the purchaser's drawings and BOM.
Steel in, galvanized tower out.
Tower fabrication and galvanizing sit side by side on the campus. Sections are cut, punched, formed and assembled in our own shop, then go straight into our own zinc bath rather than travelling to a third-party galvanizer and back.
That single decision removes the longest and least predictable step in most tower supply chains. It is also why we can hold 2,500 tonnes a month without the coating queue that constrains fabricators who buy galvanizing in.
Technical data
Specification.
Built to the purchaser's schedule. Fields marked On enquiry are issued against a specific enquiry. Delivery as per the client's requirement, confirmed with the quotation. Open the rows below for construction details, reference tables and fittings.
General
| Parameter | Specification |
|---|---|
| Products | Lattice transmission towers, M-type towers, substation gantries and equipment structures |
| Standard height | 12.8 metres and various sizes to drawing |
| Fabrication | Cutting, punching, drilling, notching, forming and assembly in-house |
| Galvanizing | Hot dip, in-house — bath up to 1 m × 7.25 m |
| Monthly capacity | 2,500 tonnes |
| Steel grade | IS 2062 structural steel — grade to drawing |
Coating
| Parameter | Specification |
|---|---|
| Standard | IS 4759:1996 coating mass; ISO 1461:2009 where specified |
| Coating mass, steel 5 mm and above | 610 g/m² minimum |
| Coating mass, steel 2 to 5 mm | 460 g/m² minimum |
| Uniformity test | IS 2633 — four one-minute copper sulphate dips |
| Adhesion test | IS 2629 — pivoted hammer and knife test |
| Fasteners | Galvanized to IS 1367 |
Reference data — what the standards requireTables from the Indian Standard, for checking any quotation against it
Coating requirements
| Product class | Minimum coating mass (g/m²) | Indicative thickness (µm) |
|---|---|---|
| Grey iron and malleable iron castings | 610 | ~86 |
| Fabricated steel 5 mm thick and above | 610 | ~86 |
| Fabricated steel 2 to 5 mm thick | 460 | ~65 |
| Fabricated steel 1.2 to 2 mm thick | 340 | ~48 |
| Threaded work 10 mm diameter and above | 300 | ~42 |
| Threaded work under 10 mm diameter | 270 | ~38 |
IS 4759 specifies coating mass, not thickness. The thickness column is a derived conversion at 7.14 g/m² per micron and is indicative only.
| Article and thickness | Local thickness min (µm) | Local mass min (g/m²) | Mean thickness min (µm) | Mean mass min (g/m²) |
|---|---|---|---|---|
| Steel above 6 mm | 70 | 505 | 85 | 610 |
| Steel above 3 up to 6 mm | 55 | 395 | 70 | 505 |
| Steel 1.5 to 3 mm | 45 | 325 | 55 | 395 |
| Steel under 1.5 mm | 35 | 250 | 45 | 325 |
| Castings 6 mm and above | 70 | 505 | 80 | 575 |
| Castings under 6 mm | 60 | 430 | 70 | 505 |
For the heaviest class the two standards agree exactly: IS 4759's 610 g/m² for steel 5 mm and above equals ISO 1461's 610 g/m² mean for steel above 6 mm.
Standard and optional fittingsWhat is supplied as standard, and what is available to order
Scope
What we supply
- Fabrication to purchaser drawings and bills of material
- Lattice towers and M-type towers
- Substation gantries and equipment structures
- Cross-arms, brackets and line hardware
- Fabricated steel items to specification
- Hot dip galvanizing of all supplied steel
- Trial assembly where specified
- Bundling, marking and dispatch to site
Process
How a tower is built
- Raw structural steel received and inspected
- Cutting and shearing to section lengths
- Punching, drilling and notching
- Forming, bending and cleat assembly
- Trial assembly where specified
- Surface preparation and acid pickling
- Hot dip galvanizing
- Coating thickness check, bundling and marking
Compliance
Standards & testing.
Routine tests are performed on every unit before dispatch. Type tests are certified from CPRI, ERDA or NABL-accredited laboratories on request.
| Standard | Scope |
|---|---|
| IS 2062 | Hot rolled medium and high tensile structural steel |
| IS 4759:1996 | Hot dip zinc coatings on structural steel and other allied products |
| IS 2629:1985 | Recommended practice for hot dip galvanizing of iron and steel |
| IS 2633:1986 | Testing uniformity of coating on zinc coated articles |
| IS 6745:1972 | Determination of mass of zinc coating |
| IS 1367 | Technical supply conditions for threaded steel fasteners |
| ISO 1461:2009 | Hot dip galvanized coatings on fabricated iron and steel articles |
| IEC 60652 | Loading tests on overhead line structures |
Inside the works
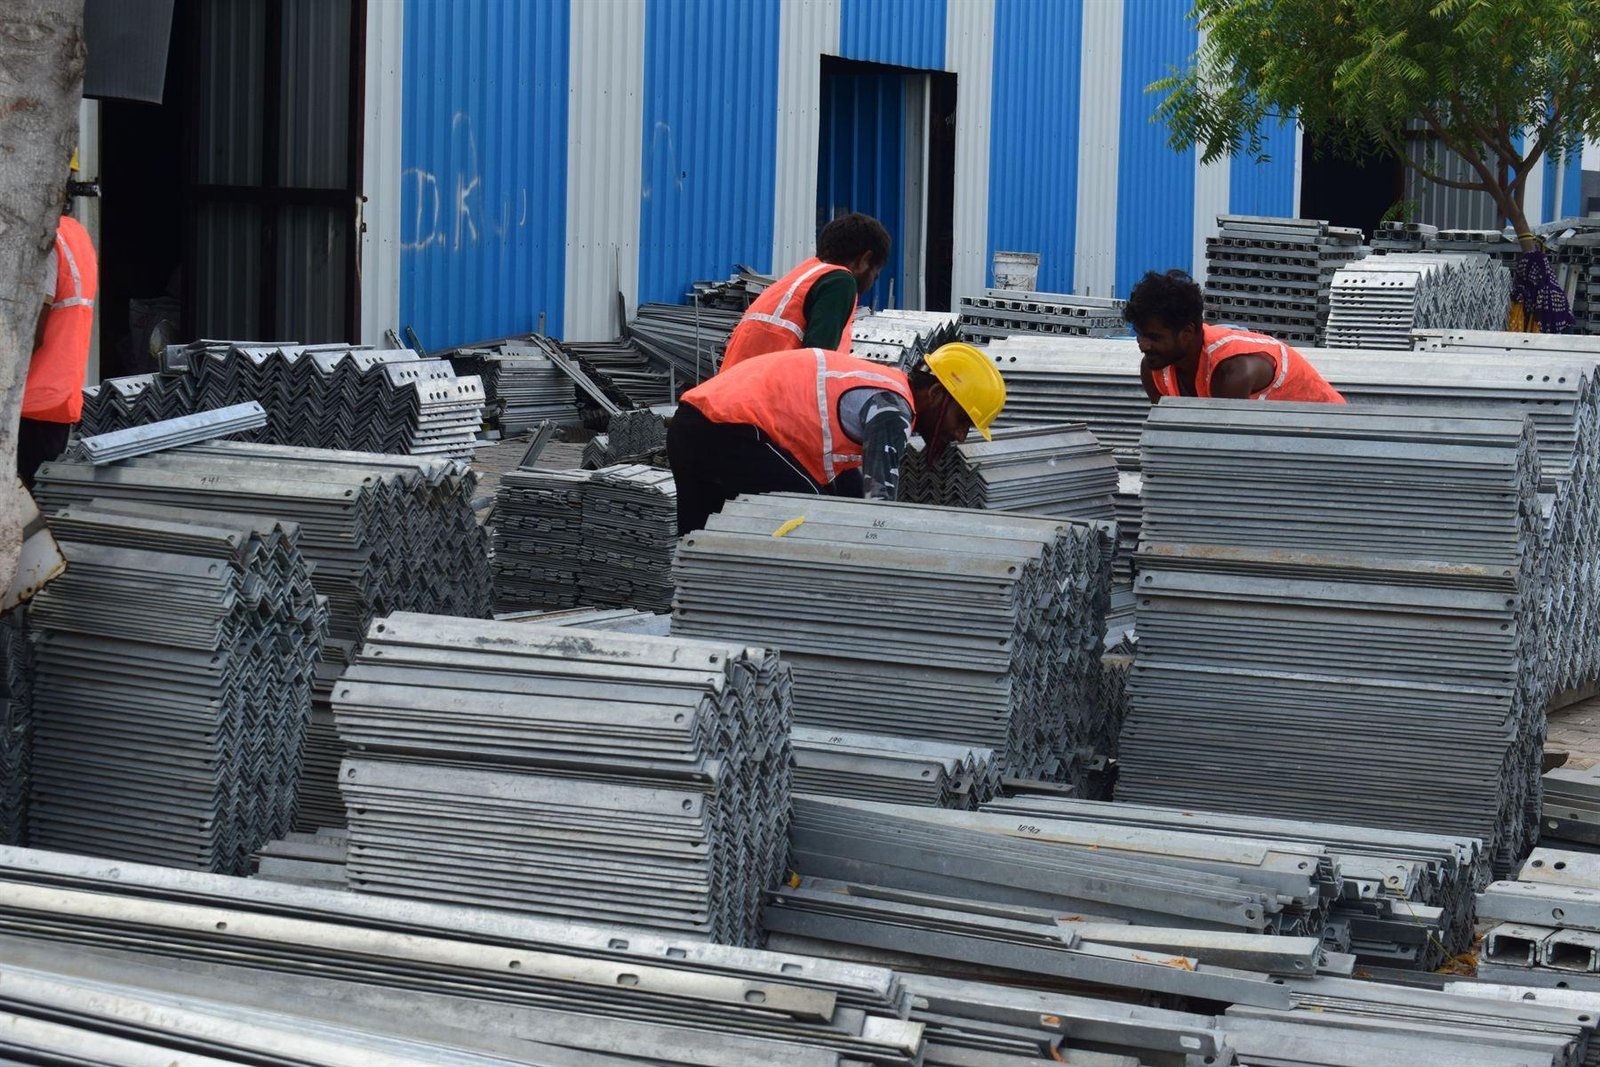
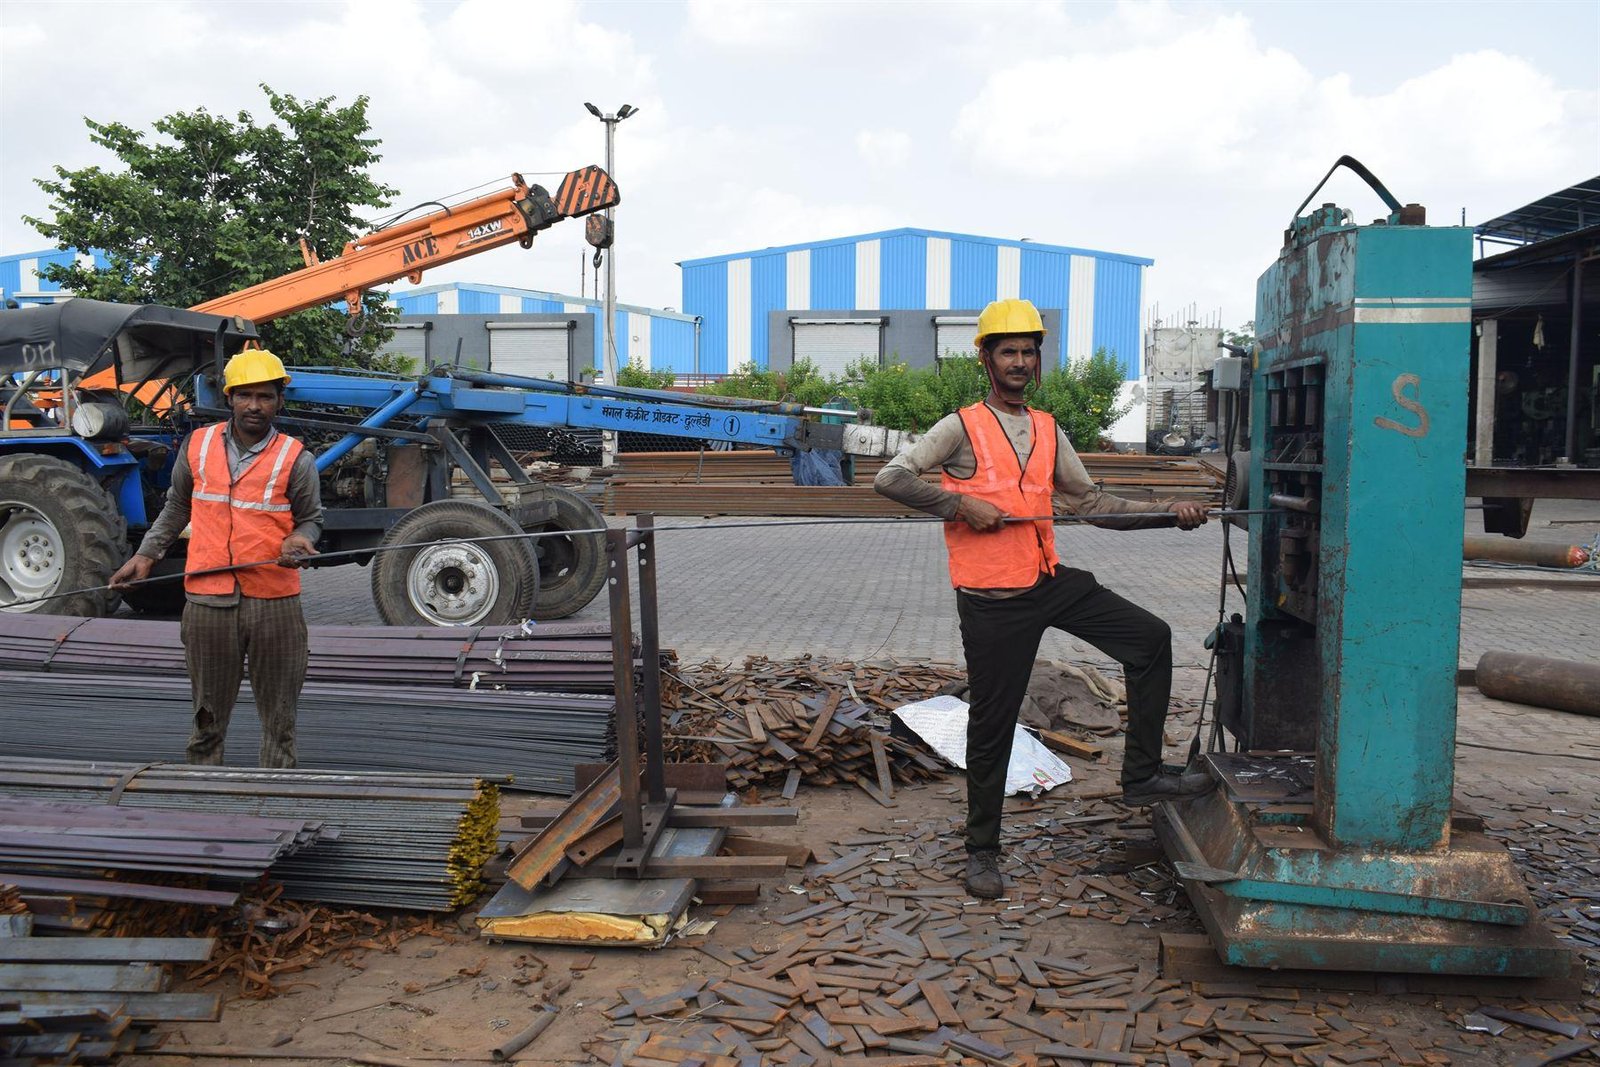
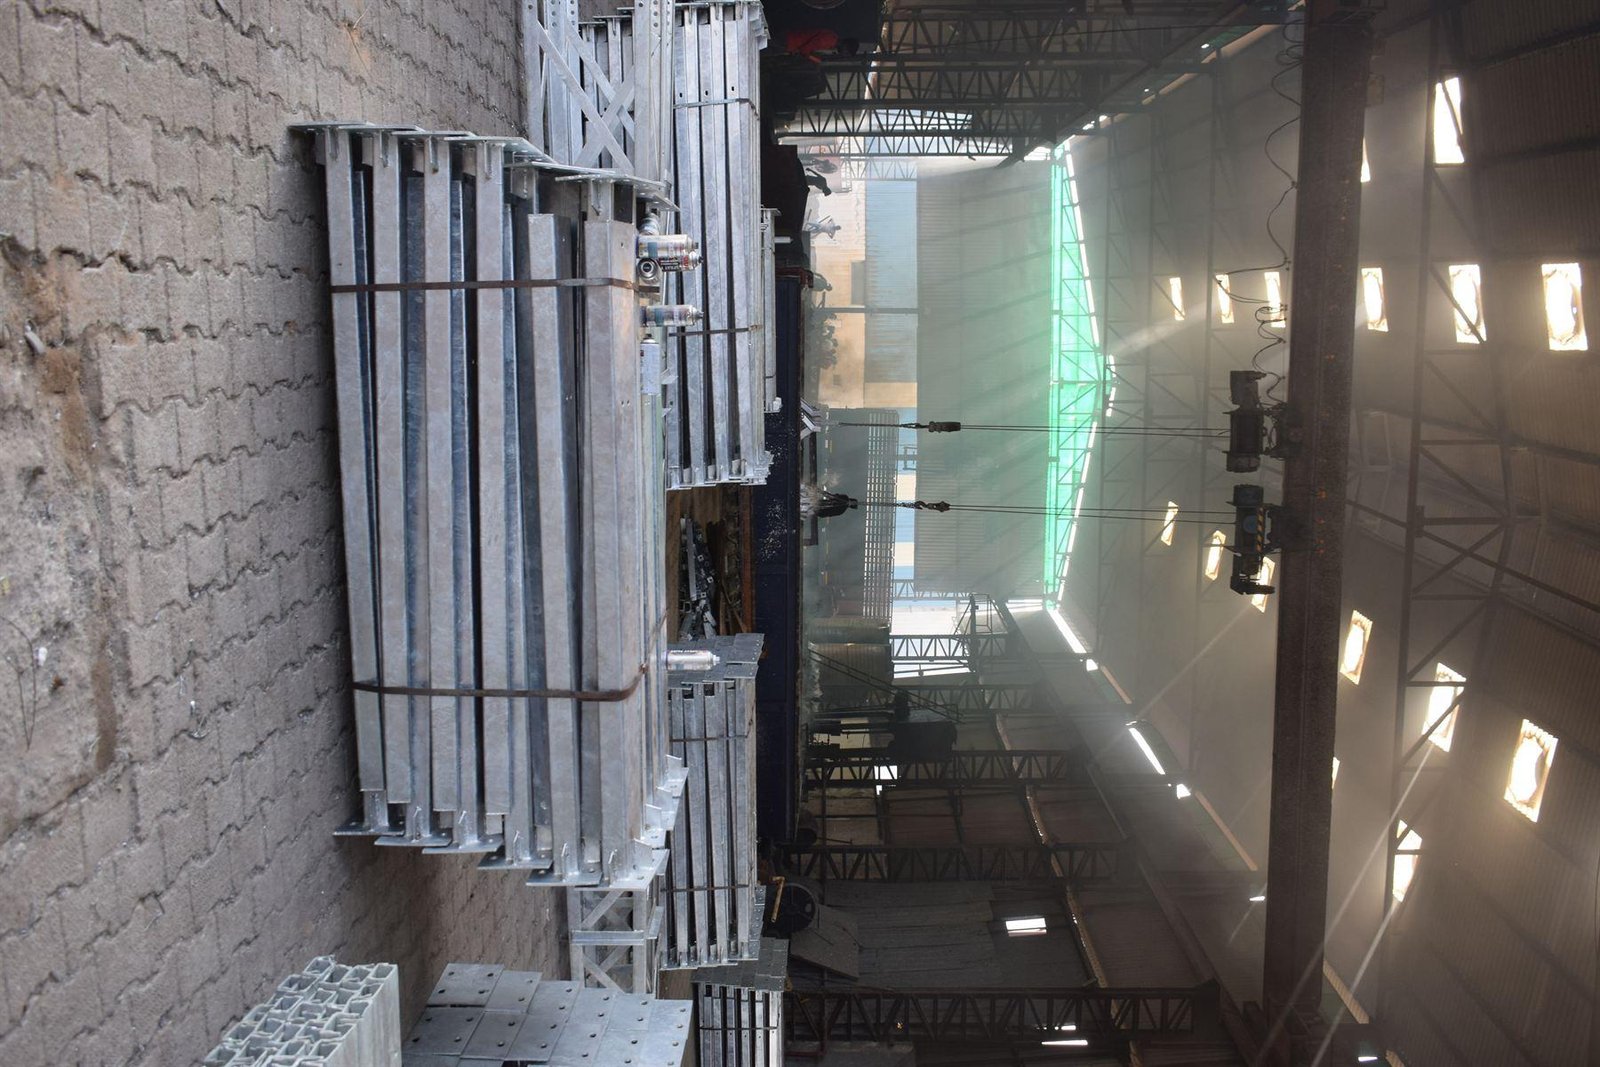
Fabrication on campus.
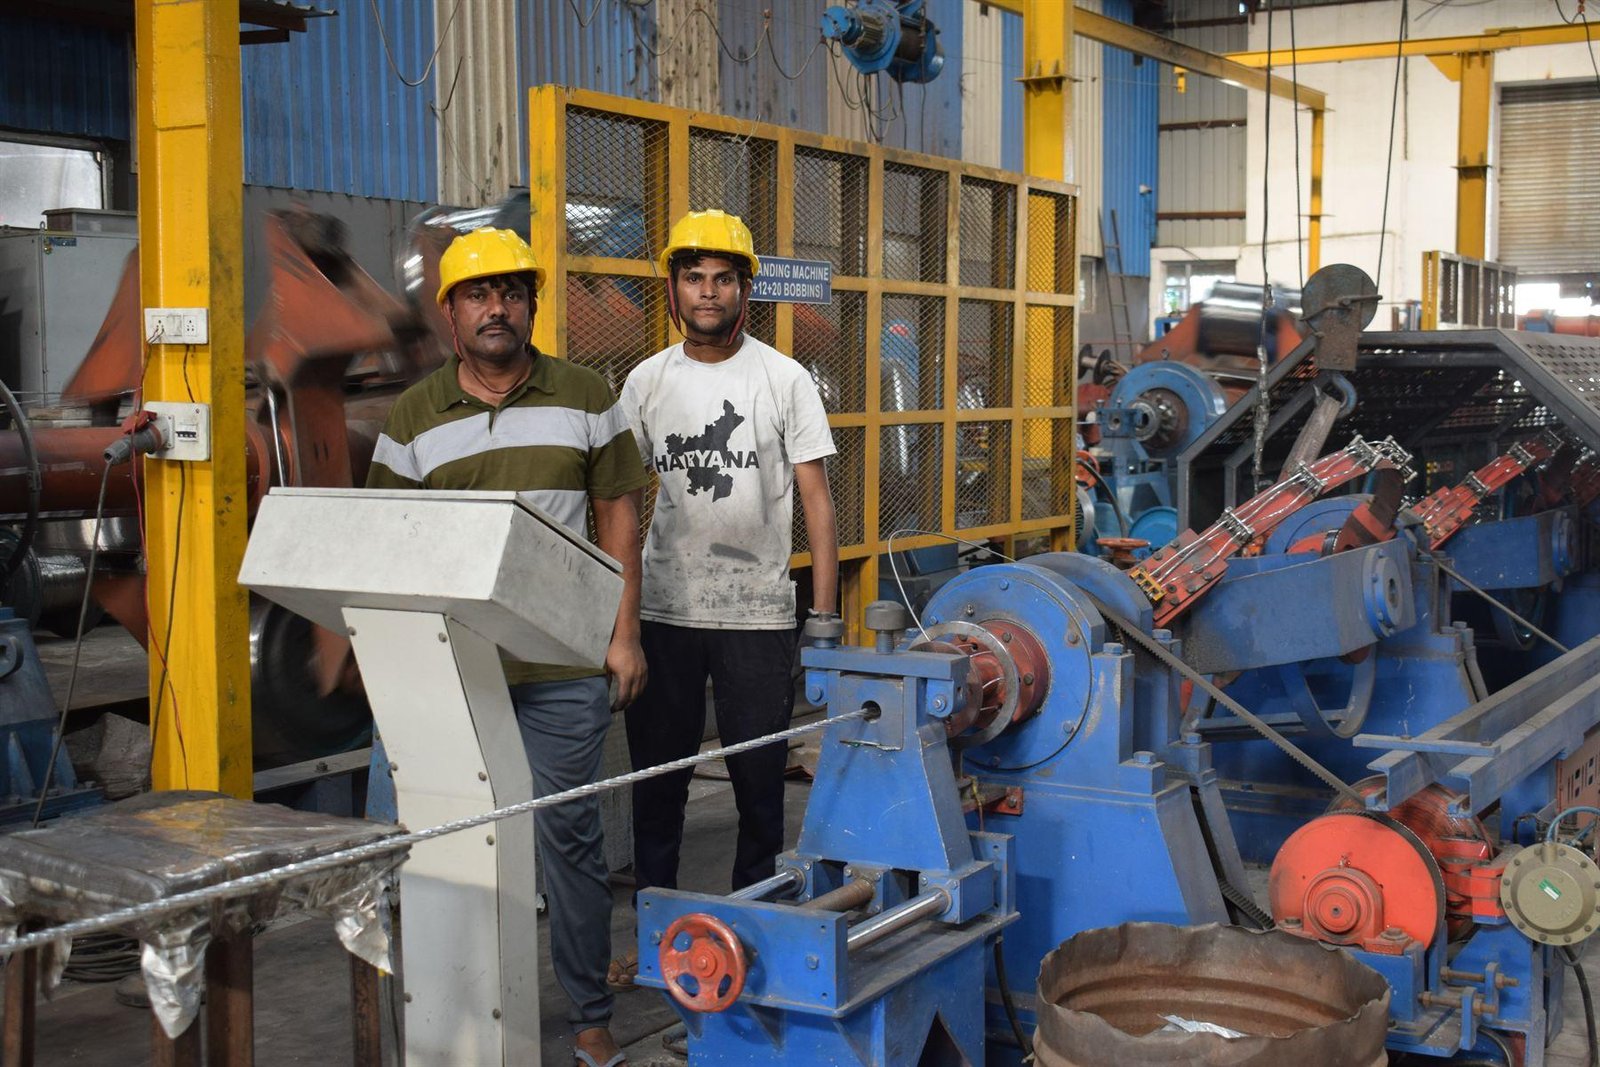
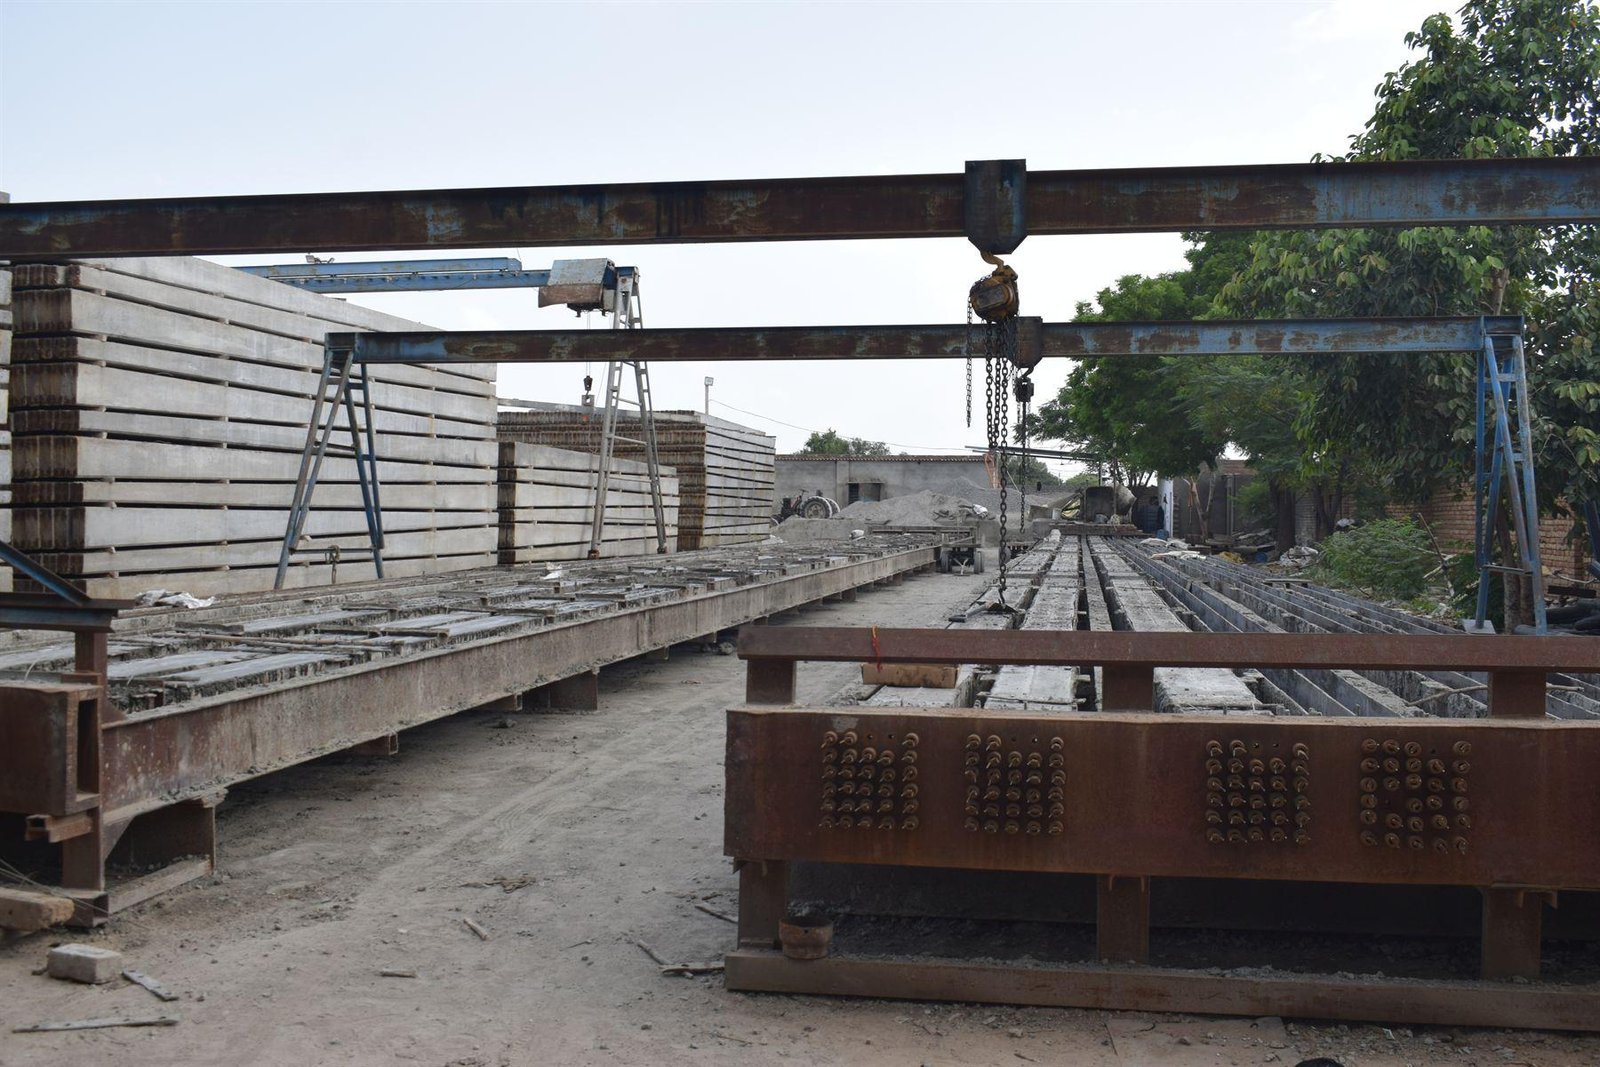
Structural fabrication and galvanizing occupy adjacent bays, so steel moves between them without leaving the site.
Walk the whole works
Applications
Where it goes to work.
Overhead lines
11 kV, 33 kV and higher transmission and distribution lines.
Structures
Gantries, equipment structures and support steelwork.
Rural electrification
Line construction under national electrification programmes.
Private networks
Captive lines for plant and industrial estate distribution.
Questions
Frequently asked.
Do you galvanize the towers you fabricate?
What is the largest section you can galvanize?
Do you design towers or only fabricate them?
Often supplied together
Send your tower drawings.
Share the type schedule, tonnage and galvanizing specification, and we will price fabrication and coating together.